
Industrial adhesive selection often slows down when teams jump straight to product names before defining the application, the line conditions, and the actual risk of failure. A structured checklist gives engineers, procurement teams, and manufacturers a repeatable way to narrow options faster, reduce avoidable trials, and make clearer decisions across technical and commercial stakeholders.
Explore industrial adhesive solutions through the lens of application fit rather than brand-first comparison. That approach usually leads to better early conversations about substrates, cure logic, environmental exposure, and process limits before samples are requested.
Why industrial adhesive selection needs a structured checklist
Adhesive selection is rarely a one-variable decision. A material that bonds well in a lab test may still fail in production because of oil residue, short open time, dispensing limits, heat cycling, or unrealistic cure expectations. In many projects, the real problem is not the adhesive itself. It is incomplete input data at the selection stage.
A checklist helps teams align around the same questions before they shortlist products. It also improves communication between engineering, sourcing, quality, production, and the adhesive manufacturer. Instead of asking for a “strong glue,” the team can define the exact bond, process, and durability target.
What this checklist helps you solve
Used properly, an industrial adhesive selection checklist can help with three common problems:
- Faster shortlisting of realistic adhesive types
- Fewer trial-and-error cycles caused by missing application details
- Better supplier communication during RFQ, sampling, and validation
It is especially useful when multiple adhesive chemistries could work on paper, but only one or two fit the actual production method and service conditions.
Define the bonding application and business goal
Start with the job the adhesive must do. Is the goal structural bonding, temporary assembly, sealing, vibration damping, gap filling, potting, or cosmetic fixing? A clear use case prevents confusion between adhesives that can bond the same substrates but deliver very different performance.
Then define the business goal behind the bond. Common examples include reducing fasteners, shortening assembly time, improving appearance, lowering rework, increasing automation, or surviving harsher field conditions. This step matters because the technically strongest bond is not always the commercially smartest choice.
Useful starting questions include:
- What two or more substrates are being joined?
- Is the bond permanent, removable, or serviceable?
- Is the adhesive replacing welding, tape, mechanical fixing, or gasket material?
- What failure would be unacceptable: leak, debond, cracking, creep, or appearance defect?
- What does project success look like in production and in service?
Confirm the substrates and surface conditions
Substrate compatibility is one of the fastest ways to eliminate unsuitable options. Metals, glass, ceramics, rubber, engineering plastics, low-surface-energy plastics, composites, and coated parts all interact differently with adhesives. Even within one substrate family, surface treatment, mold release, oxidation, texture, and contamination can change bond quality.
List each surface exactly as it appears at the bonding station, not as it appears on the drawing. For example, “powder-coated aluminum with light handling oil” is more useful than “aluminum.” Surface condition often determines whether you need a primer, abrasion, cleaning step, or a different adhesive chemistry entirely.
Teams comparing test plans may find it useful to review Practical Guide: Adhesive Testing Methods Buyers Should Understand before setting acceptance criteria, because poor test design can create misleading substrate conclusions.
Map the operating environment and service conditions
An adhesive that performs well indoors at room temperature may not survive outdoor humidity, repeated washdown, chemical splash, UV exposure, or heat aging. Service environment should be defined early, because environmental resistance is often more important than initial bond strength.
Map the main exposure factors:
- Continuous and peak operating temperature
- Humidity and water contact
- Outdoor UV exposure
- Chemical contact such as oils, fuels, cleaners, or solvents
- Thermal cycling frequency and temperature swings
- Shock, vibration, and movement during service
If the joint combines dissimilar materials, also consider differential thermal expansion. A rigid adhesive may test well at room temperature but crack under repeated expansion and contraction. In those cases, flexibility can matter more than headline strength.
Identify mechanical loads, stress types, and expected durability
Not all stress is equal. Shear, peel, tensile, cleavage, impact, and cyclic fatigue affect joints differently. Adhesives usually perform better in some stress modes than others, so the load direction and joint design must be understood before selecting a chemistry.
Ask practical questions such as:
- Will the joint carry static load, dynamic load, or occasional shock?
- Is the bond line thin and well controlled, or will it bridge gaps?
- Will the assembly flex in use?
- How many service cycles are expected?
- What is the acceptable degradation over time?
Long-term durability should be treated as a design requirement, not a bonus. If a product sees repeated stress, the wrong adhesive may pass an initial test and still fail early in service.
Match cure time, production cycle, and equipment constraints
Many adhesive projects fail not because bond performance is poor, but because the cure profile does not fit the manufacturing line. Cure speed affects labor, fixturing time, work-in-progress, throughput, and defect risk. A material that cures too slowly may block line flow. A material that cures too fast may reduce workable time and increase scrap.
Selection should account for:
- Required open time and assembly window
- Fixture time and full cure time
- One-component or two-component handling
- Heat, moisture, UV, or room-temperature cure mechanism
- Mixing and dispensing equipment available on site
For transparent substrates, fast line speeds, or small bond areas, it can be useful to compare UV adhesive options for industrial projects when the process allows light access and cure control is important.
Check process compatibility, automation needs, and line speed
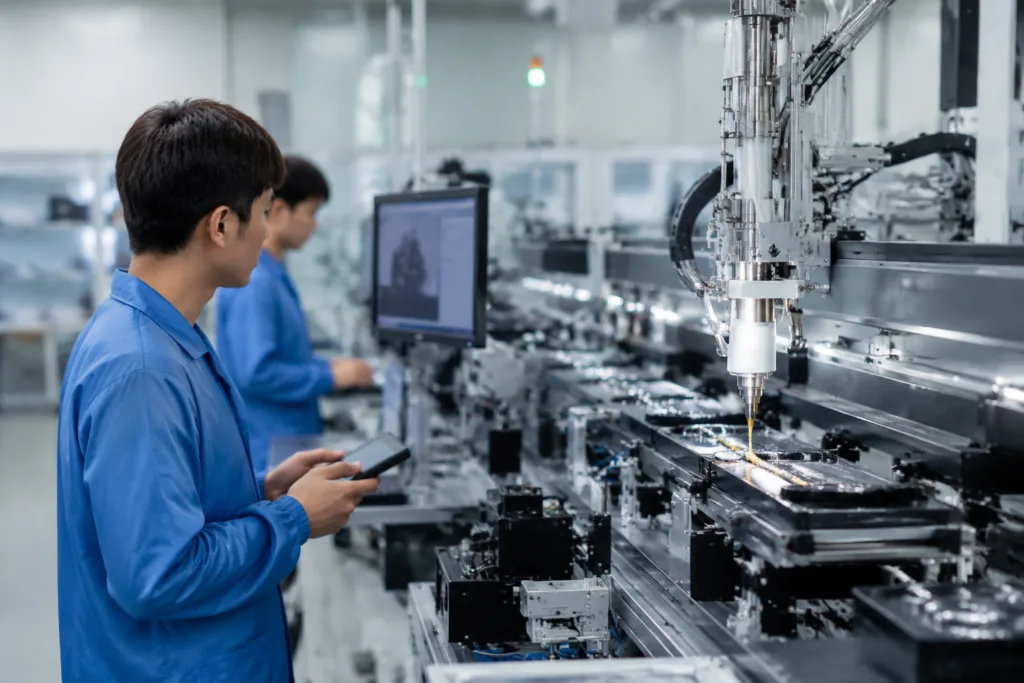
An adhesive can be technically suitable and still be a poor production choice if its viscosity, thixotropy, or application method does not match the equipment. Manual assembly, semi-automatic dispensing, and fully automated lines each create different requirements.
Review process-fit factors such as bead control, sag resistance, gap-filling ability, pumpability, mixing ratio control, and sensitivity to operator variation. If the line has short takt time, evaluate whether the adhesive can be dispensed consistently without stringing, clogging, or frequent maintenance stoppages.
From a manufacturer perspective, ZDS often sees better project outcomes when process constraints are shared early, because viscosity and cure logic are only meaningful when tied to real production equipment and cycle time.
Review regulatory, safety, and compliance requirements
Some projects need specific documentation, low-odor handling, restricted substance review, or safer processing characteristics for workers and end users. Regulatory needs vary by industry and region, so this step should focus on the actual application rather than generic assumptions.
Typical checkpoints include workplace handling requirements, end-use restrictions, transport considerations, and documentation needed for internal approval. Procurement teams should make sure these requirements are visible before samples are evaluated, not after a preferred adhesive has already been chosen.
Evaluate packaging format, storage, shelf life, and handling
Packaging affects usability more than many teams expect. Cartridge, pail, drum, syringe, dual-cartridge, and bulk systems support very different production models. The right format depends on consumption rate, mixing method, operator skill, and waste tolerance.
Also review storage temperature, moisture sensitivity, shelf life, lot traceability, and rework practicality. A high-performance adhesive may become a poor fit if its storage demands are hard to maintain across multiple sites or if expired stock creates avoidable cost.
Build a shortlist using adhesive testing criteria
Once the application inputs are defined, create a shortlist based on testable criteria rather than marketing descriptions. Good shortlists usually compare only a small number of candidates with clear reasons for inclusion. Too many samples often slow decisions without improving confidence.
Your shortlist matrix can include:
- Substrate compatibility
- Environmental resistance fit
- Stress and durability fit
- Cure profile and takt-time fit
- Dispensing and automation fit
- Safety and documentation fit
- Packaging and storage fit
- Relative cost-performance logic
When comparing supply models, it helps to read Adhesive Supplier vs Manufacturer: The 7 Critical Differences Every Buyer Should Know so the team can distinguish between a stocked product source and a formulation partner that can address process-specific requirements.
What to ask an adhesive manufacturer or adhesive supplier before sampling
Sampling goes faster when the technical conversation is specific. Instead of asking for a universal recommendation, provide the bond design, surface condition, environmental exposure, cure preference, application method, and acceptance criteria.
Useful questions include:
- Which adhesive chemistries are realistic for these substrates and why?
- What surface preparation is required for consistent results?
- What cure conditions are needed for handling strength and full performance?
- What failure modes should we expect if process control is weak?
- How sensitive is the material to bond-line thickness, mixing accuracy, or humidity?
- What test methods do you recommend for validation?
- Can the formulation or packaging be aligned with our process constraints?
Supplier comparison is stronger when teams review 7 Red Flags & 9 Buyer Criteria: How to Choose the Right Adhesive Manufacturer for Your Project before issuing samples or RFQs, especially for applications that may need ongoing technical support.
How to compare test results and avoid common selection mistakes
Comparing results is not just about choosing the highest bond number. The best candidate is the one that performs consistently under realistic conditions and fits production with acceptable risk. A lower nominal strength result may still be the better choice if it offers better toughness, easier dispensing, or more stable process performance.
Common selection mistakes include:
- Testing on clean lab coupons instead of real production surfaces
- Ignoring cure conditions used in actual manufacturing
- Overweighting initial strength and underweighting durability
- Using the wrong test method for the real stress mode
- Selecting based on unit price without considering scrap, labor, or rework
- Shortlisting too many products without clear go/no-go criteria
Document results in a simple scorecard that separates must-have requirements from nice-to-have features. That keeps one strong but irrelevant performance metric from dominating the final decision.
How a checklist improves adhesive selection efficiency across teams
A checklist standardizes what information gets collected before technical review, RFQ, sampling, and production trial. That reduces repeated questions, shortens supplier back-and-forth, and helps procurement compare options using the same decision structure as engineering.
It also creates a reusable internal record. Once a team has a solid template for industrial adhesive selection, future projects become easier to scope, especially when similar substrates, line conditions, or environmental exposures appear again.
A simple decision workflow for moving from checklist to final approval
A practical workflow can stay simple:
- Define the application, substrates, and service conditions
- Set process and cure constraints
- Identify compliance and handling requirements
- Shortlist realistic adhesive types
- Request targeted samples with test criteria
- Run validation on real surfaces and realistic conditions
- Compare technical fit, process fit, and cost-performance
- Approve the lowest-risk option for production trial
This sequence prevents late-stage surprises and makes final approval easier to defend internally.
Final takeaway
Faster and safer industrial adhesive selection depends less on finding a miracle product and more on asking the right questions in the right order. A repeatable checklist helps teams define the bond, screen out poor-fit materials early, compare suppliers more clearly, and reach approval with less avoidable risk. For most industrial projects, disciplined selection work up front saves far more time than broad sample testing later.
FAQs
What is the first step in industrial adhesive selection?
The first step is defining the exact bonding application and the business goal, including substrates, joint purpose, required durability, and what success looks like in production.
Why do substrate details matter so much when choosing an adhesive?
Substrate type, coatings, contamination, and surface energy directly affect wetting, adhesion, and long-term bond reliability, so incomplete surface information often leads to wrong shortlists.
Should teams choose adhesive products based on the highest strength value?
No, the better choice is usually the adhesive that balances realistic strength, durability, cure fit, process compatibility, and environmental resistance for the actual application.
How many adhesive samples should be tested in a typical shortlist?
A small shortlist is usually more effective, because testing a limited number of realistic candidates with clear acceptance criteria produces faster and cleaner decisions than broad unfocused sampling.
What should procurement ask before requesting adhesive samples?
Procurement should confirm substrate details, service conditions, cure needs, packaging preferences, compliance requirements, and the test criteria that will be used to compare candidates.
When is a manufacturer a better choice than a general supplier?
A manufacturer may be the better choice when the application needs formulation guidance, process-specific adjustment, packaging flexibility, or deeper technical input during validation and scale-up.
Related Reading
- How to Write an Effective RFQ for Adhesives to Get Faster, More Accurate Supplier Responses
- How to Prepare for a Custom Adhesive Quote: Essential Details for Manufacturers
- Mastering Surface Preparation for Bonding: 7 Steps That Solve 90% of Adhesive Failures
- Adhesive Strength Simplified: Peel, Shear, & Tensile Performance Decoded
- Demystifying Adhesive Curing vs Drying: 7 Traps Industrial Buyers Need to Avoid