
A rubber adhesive data sheet can look straightforward at first glance: peel strength, viscosity, cure speed, temperature resistance, and a few substrate notes. In real sourcing and engineering work, however, those numbers only become useful when you connect them to joint design, rubber type, line conditions, and service environment. This rubber adhesive TDS guide explains how we read technical data sheets from a manufacturer’s perspective so engineers, procurement teams, and technical buyers can compare options more confidently and avoid choosing a product on one impressive headline value.
If your project involves dynamic rubber joints, oil exposure, mixed substrates, or production-line curing limits, rubber adhesive manufacturing support for demanding bonding projects becomes important long before final purchasing. In our work, that usually means looking beyond nominal bond strength and helping customers evaluate viscosity, flexibility, primer needs, cure window, packaging format, and batch-to-batch consistency so the adhesive fits both the elastomer and the real manufacturing process.
What a Rubber Adhesive TDS Can Tell You—and What It Cannot
A TDS is a screening document. It helps you narrow the field, compare product families, and spot obvious mismatches. It can tell you whether an adhesive is solvent based, moisture curing, two-part reactive, pressure sensitive, or heat activated. It may also show viscosity range, solids content, recommended substrates, hardness after cure, elongation, peel or shear values, and storage guidance.
What it usually cannot tell you on its own is whether the adhesive will survive your exact duty cycle. Rubber bonding performance changes significantly with elastomer family, filler package, mold release residue, surface texture, bond-line thickness, cure schedule, and whether the joint sees peel, cleavage, compression, or cyclic flex. That is why buyers comparing products should combine TDS review with sample trials and process checks.
When customers ask us to compare candidate materials, we usually start with application geometry, substrate pair, flex demand, temperature range, chemical contact, assembly takt time, and failure mode target. That practical framework matters more than any single advertised value.
Why Rubber Adhesive Selection Should Not Depend on Lap Shear Alone
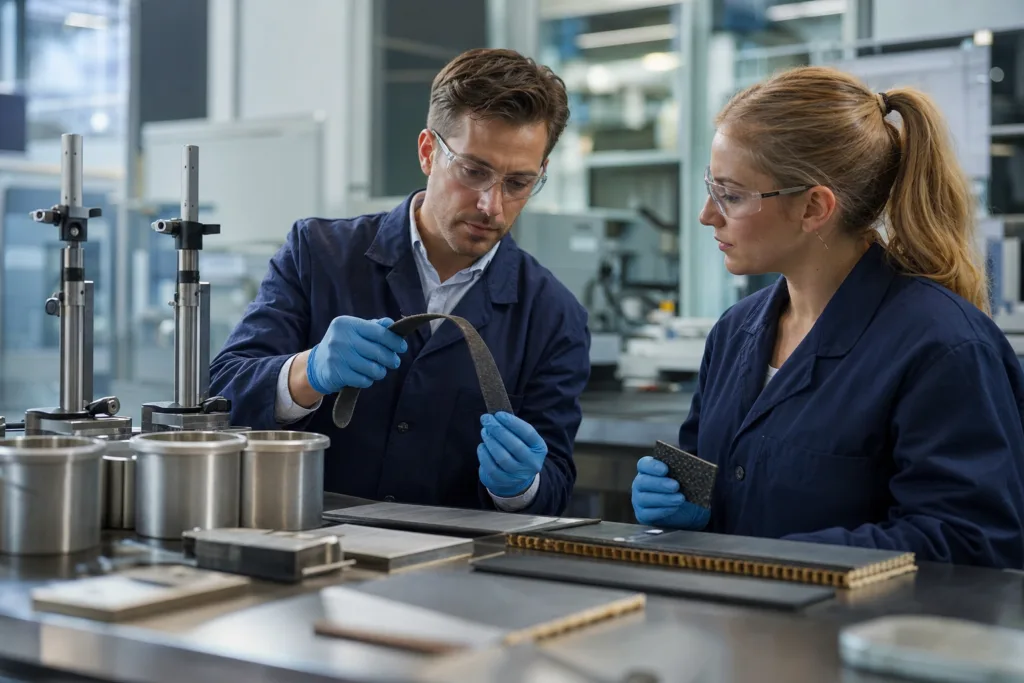
Lap shear is one of the most misunderstood values in adhesive comparison. It is useful, but only within context. A high shear number can look attractive in a table while saying very little about a flexible rubber assembly that is repeatedly bent, peeled, or exposed to oil.
Many TDS documents show shear results from metal-to-metal or rigid test setups because these are easier to standardize. The challenge is that a rubber-to-metal, rubber-to-plastic, or rubber-to-rubber joint behaves differently. Soft substrates deform, distribute stress differently, and may fail cohesively, adhesively, or by tearing the rubber itself.
When reviewing shear values, check the test method, substrate, cure condition, dwell time, and failure description. A result tied to an ASTM D1002 lap shear strength test is only comparable to another value if specimen design and preparation are reasonably aligned. Otherwise, buyers can end up comparing numbers that look similar but come from different test realities.
For broader decision-making, we often advise customers to combine shear review with rubber bonding adhesive guidance for metal, glass, and plastic applications so they can match the adhesive not only to the substrate but also to movement, contamination risk, and operating conditions.
Peel Strength and Flexible-Joint Performance
For many rubber assemblies, peel resistance is more important than maximum shear strength. Gaskets, trim, vibration pads, soft sleeves, elastomer covers, and flexible laminates often fail from edge lift or progressive peel rather than pure tensile loading.
Peel data helps you understand how the bond behaves when stress concentrates at the bond front. A strong peel result often indicates better stress distribution, better wetting of the substrate, and a cured adhesive film that can move without becoming brittle. That matters when the rubber stretches, the bonded part is repeatedly flexed, or service loads are not perfectly aligned.
Still, peel numbers must be interpreted carefully. Check whether the test was 90-degree or 180-degree peel, whether the substrate was rigid or flexible, and whether the failure was adhesive or substrate tear. Substrate tear can be a positive sign, but it can also hide the fact that one rubber grade was weaker than another. In comparison work, similar test setup matters more than the absolute number alone.
We also look at elongation, modulus, and cured-film feel when evaluating flexible-joint performance. An adhesive can show acceptable peel in the lab yet crack in production if it is too hard for the assembly’s movement profile. That is why some projects benefit from reviewing alternatives such as ZDS-8202AB permanent anti-yellowing PU adhesive for flexible bonding when flexibility and stress absorption matter more than rigid structural strength.
Tensile, Shear, and Elongation Data
Rubber adhesive TDS documents may list tensile strength, elongation at break, modulus, or hardness of the cured adhesive itself. These values do not directly equal bond strength, but they tell you how the cured polymer is likely to behave inside the joint.
| TDS Property | What It Suggests | What Buyers Should Check |
|---|---|---|
| Peel strength | Resistance to edge-lift and progressive debonding | Peel angle, substrate, dwell time, failure mode |
| Lap shear | Load-bearing under overlap tension | Test method, rigid vs flexible substrates, surface prep |
| Tensile strength | Cohesive strength of cured adhesive | Whether the joint will actually see tensile loading |
| Elongation | Ability to stretch before failure | Balance with modulus and recovery, not just high percentage |
| Hardness | Relative stiffness of cured film | Whether hard cure could stress soft elastomers |
| Viscosity | Flow, wetting, and dispensing behavior | Application method, gap, sag, and coverage uniformity |
Higher elongation is not always better. A very soft adhesive may tolerate movement well but creep under constant load or lose edge definition. A very hard adhesive may show good initial handling but fail under repeated bending. The right balance depends on the assembly. In practice, we compare tensile, elongation, and hardness together rather than treating any one value as decisive.
Oil, Heat, and Chemical Resistance
Oil resistance is a major selection factor for rubber adhesives used in automotive parts, machinery seals, rollers, hoses, and protective assemblies. But a TDS statement such as “good oil resistance” is too broad for purchasing decisions. Buyers should ask which oils, what temperature, how long, and whether the result refers to appearance, weight change, softening, or retained adhesion.
The same caution applies to chemical resistance and heat resistance. A cured adhesive may survive intermittent temperature spikes but lose flexibility after long thermal aging. It may tolerate splash exposure but not full immersion. It may resist mineral oil better than synthetic lubricants or fuel-related fluids.
For production evaluation, we recommend building a simple matrix: fluid type, temperature, exposure mode, duration, and pass/fail criterion. If the product is expected to retain bond after oil soak, do not rely on an unqualified resistance note in the TDS. Request post-aging bond data or run comparative trials.
Heat resistance should also be interpreted with the bond-line in mind. Thermal expansion mismatch between rubber and rigid substrates can create peel stress during heating and cooling cycles. Adhesives that look acceptable in static aging may still fail after thermal cycling because flexibility retention was not sufficient.
Cure Speed, Viscosity, and Process Window
One of the most practical sections in any TDS is the process information. Cure mechanism, open time, tack development, fixture speed, and viscosity affect line efficiency as much as final bond performance.
For fast-moving production, buyers should distinguish between several time concepts:
- Open time: how long the applied adhesive remains bondable before assembly.
- Pot life: for multi-part systems, how long the mixed material remains usable.
- Fixture time: how quickly parts can be handled without shifting.
- Full cure: when the adhesive reaches mature properties.
A TDS may present a cure speed achieved under ideal lab temperature and humidity. Real lines often run cooler, drier, hotter, or with different bond thickness. Rubber surfaces may also reduce or delay cure depending on additives and contamination. This is why our teams often recommend pilot testing instead of assuming the listed cure profile will transfer directly.
Viscosity matters just as much. Low-viscosity materials can wet rough or porous surfaces well, but may run, soak, or create squeeze-out. High-viscosity materials can help with gap filling and placement control but may reduce surface wetting or trap air. Buyers evaluating multiple options often benefit from adhesive selection technical support for reading performance data because the same viscosity number can behave differently depending on shear-thinning, temperature, and dispensing equipment.
Elastomer-Specific Compatibility Notes
Not all rubber is the same, and a generic “rubber compatible” statement is not enough for serious comparison. NBR, EPDM, SBR, CR, natural rubber, silicone rubber, and fluorinated elastomers present very different surface energies, additive packages, and service environments.
As a screening rule, NBR may be chosen where oil resistance is important, while EPDM is often used for weather and water exposure. Those substrate choices already hint at the adhesive demands. An adhesive suitable for one elastomer family may underperform on another because the surface chemistry, extractables, or flexibility requirements differ.
When a supplier provides bond-strength values for rubber-to-rigid assemblies, the test method should be identified. That is why it is useful to review references such as the ASTM D429 adhesion test for rubber-to-rigid substrates when interpreting whether an adhesion number is truly comparable across products, rubbers, and surface preparations.
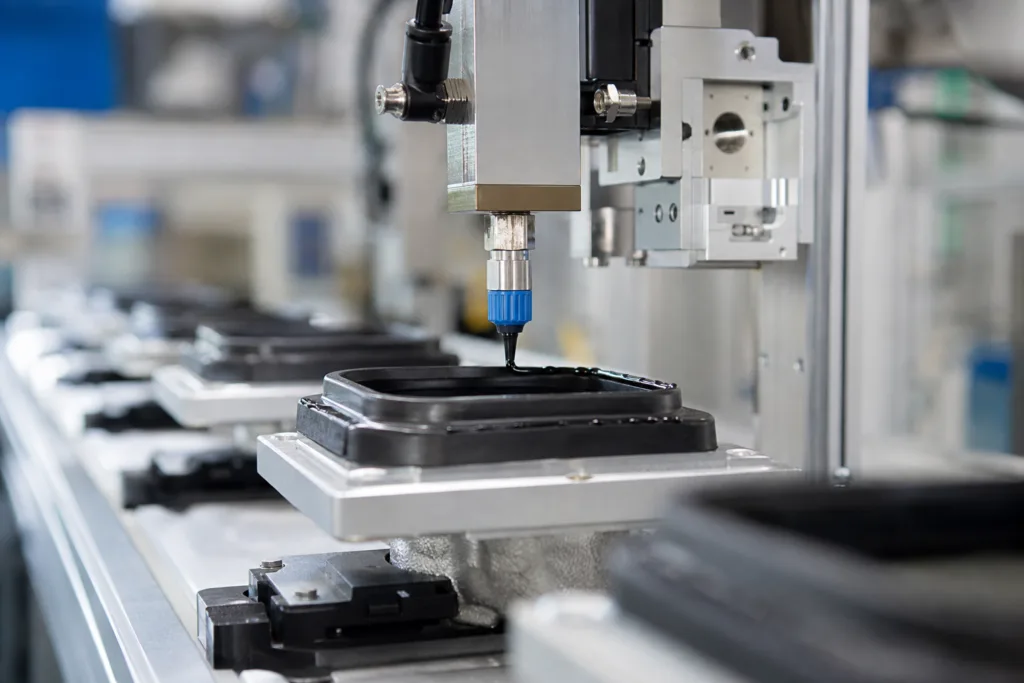
In development projects, we frequently advise customers to state the exact rubber grade, not only the elastomer family. Plasticizer level, filler content, cure package, hardness, and release chemistry can all alter bonding behavior. If the assembly involves a difficult elastomer, mixed substrates, or a nonstandard process, custom adhesive formulation support for substrate-specific requirements may be more realistic than trying to force a standard product into a marginal fit.
How Surface Preparation and Primer Use Affect TDS Results
Two buyers can test the same adhesive and get very different results because surface preparation was different. TDS values are usually generated on controlled specimens with defined cleaning and application conditions. Production parts are often less forgiving.
Common causes of inconsistency include mold release residue, dust, oil film, low-energy surfaces, oxidation, moisture, and inconsistent abrasion. On rubber parts, the problem is often subtle: the surface may look clean while still carrying ingredients that interfere with wetting or cure.
Primer use can greatly change adhesion, especially on difficult elastomers or metals exposed to corrosion risk. However, adding a primer changes process cost, line complexity, storage management, and rework handling. A TDS that lists excellent strength “with primer” should not be compared casually with a primerless system if your process does not allow that extra step.
From our manufacturing perspective at ZDS, this is one of the most common points where lab success fails to scale. We encourage customers to define the actual cleaning method, drying time, primer step, and operator window before they accept a TDS value as production-relevant.
A Practical TDS Comparison Checklist for Rubber Adhesives
When procurement and engineering are comparing several rubber adhesives, a short structured checklist saves time and prevents number-driven mistakes. We recommend reviewing the following items side by side:
| Comparison Item | Why It Matters | Decision Question |
|---|---|---|
| Rubber type tested | Compatibility can vary sharply by elastomer family | Was the data generated on the same or similar rubber? |
| Mating substrate | Metal, plastic, fabric, and rubber each change adhesion behavior | Does the TDS reflect your actual substrate pair? |
| Test method | Numbers are not comparable without method context | Is peel, shear, or tensile the right metric for the joint? |
| Surface prep | Cleaning and abrasion can dominate the result | Can your line reproduce the stated prep? |
| Cure schedule | Different temperatures and humidity affect outcome | Does the line support the required cure window? |
| Viscosity and application | Controls wetting, coverage, and handling | Will it brush, spray, roll, or dispense reliably? |
| Flexibility after cure | Important for dynamic joints and mismatch stress | Will the cured film move with the assembly? |
| Resistance profile | Oil, heat, water, and chemicals affect durability | Which exposures are proven versus assumed? |
| Packaging and shelf life | Impacts waste, line replenishment, and storage planning | Does supply format match your usage rate? |
| QC consistency | Production stability matters more than one good sample | Can the supplier maintain batch consistency? |
Common Misreads That Lead to Bond Failure in Production
Several recurring TDS misreads cause avoidable failures.
Confusing adhesive strength with joint reliability
A high bond-strength number does not guarantee survival under peel, vibration, flex fatigue, or thermal cycling.
Ignoring the tested substrate
Data generated on grit-blasted steel may not predict behavior on plated metal, painted components, or low-energy plastics.
Treating “room-temperature cure” as one fixed condition
Ambient cure can vary widely with humidity, adhesive thickness, and air circulation.
Overlooking failure mode
Substrate tear, cohesive failure, and adhesive failure each tell a different story. Without failure mode information, comparison is incomplete.
Assuming chemical resistance statements are universal
Oil resistance in one lubricant class does not automatically mean resistance in fuel, solvent, or hot hydraulic fluid exposure.
How to Match TDS Data to Your Actual Rubber Bonding Application
The most reliable way to use a TDS is to convert it into an application decision path. Start with the real assembly, not the product brochure. What materials are being joined? Is the joint flexible or rigid? Does it see peel at the edge? Is the line manual or automated? How fast must handling strength develop? Which fluids or temperatures matter most?
Then shortlist the properties that truly control success. For a rubber seal bonded to metal, peel retention after heat and oil aging may matter more than raw shear. For a soft laminate, low modulus and good wetting may matter more than hardness. For a fast-moving assembly line, open time and fixture speed may dominate.
We usually suggest a staged evaluation: first TDS screening, then lab sample comparison, then pilot-line verification, then supply and QC review. This approach keeps engineering, sourcing, and manufacturing aligned. It also makes buyer conversations with suppliers more efficient because the key unknowns are identified early rather than after a failed trial.
For more complex elastomer projects, we often help customers convert general requirements into specific test plans: pre-conditioning, oil soak, peel-after-aging, thermal cycle, and visual failure analysis. That process is often more informative than requesting one more headline strength figure.
How ZDS Helps Customers Interpret Rubber Adhesive Data in Application Context
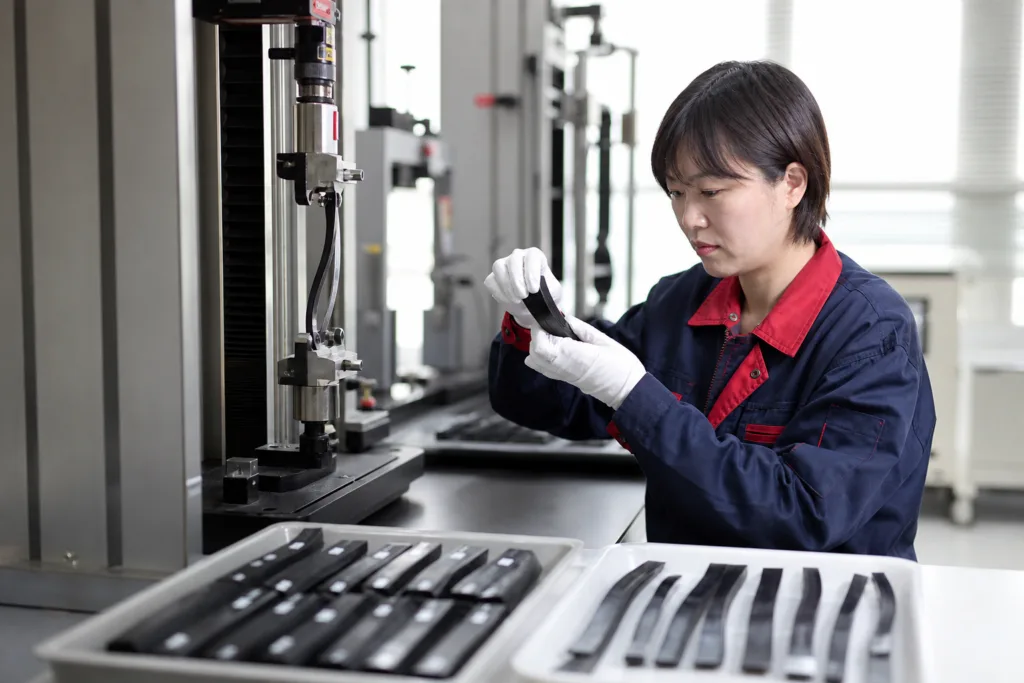
At ZDS, we approach rubber adhesive evaluation as a matching problem between chemistry, substrate, process, and service environment. That means we do not stop at the TDS table. We look at whether the adhesive’s viscosity matches the dispensing or coating method, whether the cure profile fits takt time, whether the cured film can absorb movement, and whether the packaging format supports stable plant use.
In OEM and private label work, the question is often not just “Which adhesive works?” but “Which adhesive works consistently at scale?” That brings in formulation stability, raw-material control, pilot sampling, packaging choice, shelf-life management, and communication between technical and sourcing teams. A useful TDS should support those decisions, but production validation completes the picture.
For buyers comparing suppliers, the strongest signal is usually not the highest isolated number. It is a combination of clear test context, honest limitations, relevant samples, and a practical path to line validation. When those pieces are in place, the TDS becomes a decision tool rather than a marketing sheet.
Conclusion
A good rubber adhesive TDS guide is really a guide to asking better questions. Peel, flexibility, oil resistance, cure speed, and substrate compatibility all matter, but only when interpreted against the real joint, the real rubber, and the real production method. The most dependable selection process is to use the TDS for disciplined screening, then verify the fit with targeted testing and application review. That is how buyers reduce risk, compare formulations fairly, and choose a rubber adhesive that performs beyond the lab sheet.
FAQs
What is the most important number in a rubber adhesive TDS?
There is rarely one single most important number. The right priority depends on the application. For flexible rubber joints, peel resistance, elongation, and cured-film flexibility may matter more than lap shear. For oil-exposed assemblies, retained performance after fluid aging can be more valuable than initial strength. The best approach is to identify the real failure risk first and then read the TDS around that risk.
Why can two rubber adhesives with similar shear strength perform very differently?
Similar shear values can hide major differences in peel behavior, flexibility, cure profile, and substrate wetting. Two products may also have been tested on different substrates or with different surface preparation. In production, those differences affect edge lift, fatigue resistance, and durability, so the same headline number does not guarantee comparable field performance.
How do I know whether a rubber adhesive is compatible with EPDM, NBR, or SBR?
Start by checking whether the TDS names the elastomer family and the mating substrate used in testing. Then confirm whether primers, abrasion, or heat activation were required. Compatibility should ideally be verified with your exact rubber grade because fillers, plasticizers, and release residues can change bonding behavior significantly even within the same elastomer family.
Should procurement teams request samples even if the TDS looks strong?
Yes. A strong TDS is useful for screening, but samples are essential for validating wetting, dispensing behavior, cure speed, and bond retention under your process and service conditions. Sample trials also reveal practical issues such as odor, squeeze-out, operator window, and packaging suitability that may not be obvious from the data sheet alone.
When does custom formulation make sense for rubber bonding?
Custom formulation becomes worthwhile when standard products are close but not fully suitable. Typical triggers include difficult elastomers, mixed substrates, unusual viscosity needs, faster or slower cure targets, specific oil or heat exposure, or packaging constraints for automated lines. In those cases, adjusting the formulation can be more effective than forcing a generic adhesive into a marginal application.
Can a rubber adhesive TDS predict long-term production reliability?
Not by itself. A TDS provides valuable baseline information, but long-term reliability depends on process control, surface preparation, bond design, environmental exposure, and manufacturing consistency. The most reliable prediction comes from combining TDS review with comparative testing, pilot-line validation, and supplier quality evaluation.
Related Reading
- how to choose the right industrial adhesive for your application
- practical guide to adhesive testing methods buyers should understand
- why lap shear alone is not enough in adhesive joint evaluation
- a practical industrial adhesive selection checklist for faster decisions
- polyurethane adhesive solutions for flexible industrial bonding