
In electrical assemblies, insulation performance is not only about dielectric properties. It is also about where the material goes, where it stops, and how consistently it covers the target area without migrating into pads, test points, connectors, vents, moving parts, or other sensitive features. That is why insulation adhesive viscosity is often one of the first screening criteria when engineers and buyers review insulation adhesive solutions for controlled component protection. A material that flows too freely can flood critical areas. A material that is too resistant to flow may leave voids, thin edges, or incomplete wetting that weakens electrical protection.
For production teams, the practical question is not simply whether an adhesive is conductive or non-conductive. The real question is whether its rheology matches the assembly geometry, dispense method, line speed, cure window, and protection goal. Viscosity, yield stress, and shear response all affect bead shape, edge containment, gap penetration, and final coverage. As explained in Viscosity, yield stress, and flow behavior in adhesive selection, flow behavior is a broader topic than a single viscosity number, which is why two insulating adhesives with similar catalog descriptions can behave very differently on the same PCB or electrical component.
Why Flow Behavior Matters in Electrical Protection Applications
Insulating adhesives are often used to protect localized areas rather than fully encapsulate the whole assembly. Typical goals include preventing shorting, stabilizing wires or components, adding environmental protection, sealing against moisture entry, and controlling air gaps around energized features. In these use cases, uncontrolled spread can create new risks while trying to solve the original one.
Examples of flow-sensitive electrical applications include:
- PCB edge or corner bonding near fine-pitch pads
- Localized insulation around pins, solder joints, and terminals
- Adhesive dams or barriers near connectors
- Coil, transformer, and lead-wire stabilization
- Battery pack insulation in confined clearances
- Moisture protection around power modules and sensor housings
When adhesive floods a restricted area, it can interfere with mating connectors, cover test pads, wick under components, reduce rework access, or trap contamination. When it does not flow enough, exposed edges and unfilled paths may remain vulnerable to moisture, tracking, vibration, or dielectric breakdown. Good flow control is therefore a process-control issue, a reliability issue, and a sourcing issue.
What Insulation Adhesive Viscosity Means in Real Production Terms
In a technical data discussion, viscosity is often presented as a measured value under defined conditions. In production, however, teams usually experience it as behavior: how fast the material dispenses, whether the bead stands or slumps, how far it spreads after placement, whether it wets the substrate, and how sensitive it is to temperature or shear during dispensing.
Several practical points matter:
- Low apparent viscosity usually means easier flow into gaps and around complex surfaces, but also greater risk of migration.
- Medium viscosity may balance wetting and shape retention for many localized bonding and protective tasks.
- Thixotropy means the material may thin under shear during dispensing and then recover body after placement, helping it stay where applied.
- Yield stress affects whether the material starts moving under its own weight or remains stable at edges and vertical surfaces.
- Temperature sensitivity can change real line behavior even when the product name stays the same. Cooler materials may dispense more slowly; warmer materials may spread further.
For this reason, a single catalog viscosity value should not be treated as complete process proof. As noted by NIST in its publication on how viscosity changes with temperature and shear, non-Newtonian materials can behave differently depending on measurement and use conditions. Buyers should therefore ask not only for the nominal property, but also for the test method, temperature, and whether the material is shear-thinning or thixotropic.
Low-Viscosity vs Medium-Viscosity vs Thixotropic Insulating Adhesives
There is no universal best viscosity range for all insulation jobs. The useful choice depends on whether the job requires penetration, contour coverage, bead retention, or selective placement near sensitive features.
| Flow profile | General advantages | Common concerns | Typical fit |
|---|---|---|---|
| Low viscosity | Good wetting, easier gap entry, can reach tight spaces | Higher risk of bleed, edge spread, flooding, and wicking | Fine gap infiltration, conformal localized coverage where containment is built into design |
| Medium viscosity | Balanced coverage and control, often easier to tune for standard dispensing | May still slump on warm surfaces or wide clearances if geometry is open | General electronics protection and controlled bead application |
| High viscosity or thixotropic | Better edge definition, reduced running, improved placement on vertical or uneven areas | Can leave voids or poor wetting if substrate energy is low or shot size is too small | PCB edge control, localized dams, bonding near pads, connectors, and fine features |
For example, a low-flow option such as ZDS-3533 transparent high-thixotropy PCB adhesive may be more suitable when a stable bead is needed close to fine electronic features. By contrast, a more freely flowing material such as ZDS-168ab-1 low-viscosity insulating waterproof adhesive for electronics may be worth reviewing when wetting and penetration into tighter paths are more important than sharp bead retention. Final suitability still depends on the actual substrate, clearance, dispense pattern, and cure conditions.
How Flow Control Affects Coverage, Insulation, and Process Reliability
Electrical protection depends on uniform coverage, but uniform does not mean maximum spread. A controlled adhesive must reach the required surfaces, maintain adequate thickness where insulation is needed, and stop before it interferes with nearby functions.
Flow control influences reliability in several ways:
- Coverage continuity: better wetting can reduce exposed edges and micro-voids.
- Thickness retention: excessive spread can thin the adhesive film below the intended protective level.
- Feature isolation: stable rheology helps keep material away from conductive pads, sockets, and moving interfaces.
- Repeatability: consistent bead profile supports more predictable automated inspection and downstream curing.
- Process yield: less overflow means less cleaning, less scrap, and fewer hidden defects.
In many electronics lines, the best process outcome comes from balancing two opposing needs: enough flow for intimate surface contact, but enough body to resist uncontrolled migration after dispense.
Risks of Over-Flow Around Pads, Gaps, and Connectors
Overflow is not just a cosmetic defect. In electrical assemblies it can create assembly, service, and reliability issues that are expensive to correct later. Sensitive zones often include exposed copper, contact points, connector latches, pressure-fit areas, vent paths, and any location that requires later probing, rework, or heat dissipation.
Common overflow mechanisms include:
- Adhesive warming up during the shift and becoming more mobile
- Dispense pressure or time set too high for the selected nozzle and material
- Open bond geometry with no physical stop for the adhesive front
- Large gaps or channels that encourage capillary movement
- Long open time before gel or fixture, allowing the bead to keep moving
- Board tilt, component height variation, or vibration after dispense
A non-conductive adhesive around pins or leads can also wick unexpectedly along interfaces if surface energy is favorable. Even when the chemistry is electrically insulating, uncontrolled movement can still block mating operations or contaminate critical contact zones.
Risks of Poor Wetting and Incomplete Coverage
At the opposite extreme, insufficient flow can also create failure risk. If the adhesive bridges over roughness, trapped air, or narrow valleys without wetting them, the assembly may show apparent coverage from above while hidden voids remain below. Those voids can become moisture paths or stress concentrators.
Poor wetting is more likely when:
- The adhesive is too viscous for the feature size
- The substrate has low surface energy or contamination
- The shot size is too small to develop proper contact area
- The dispense pattern leaves unconnected islands instead of a continuous barrier
- The material begins to set before it has leveled into the intended zone
Engineers should therefore assess both edge containment and surface contact. A neat-looking bead is not enough if the underside of the bond line or the interface around fine features is not actually protected.
How Adhesive Spreading on PCB Surfaces Impacts Electrical Protection
PCB surfaces are especially sensitive because they combine mixed topography, solder mask, metallic pads, standoff gaps, and narrow spaces between components. Adhesive spreading on a flat coupon rarely predicts exactly what will happen on a populated board.
Important PCB-specific considerations include:
- Solder mask and exposed metal can show different wetting behavior
- Residues from flux, cleaning, or handling can shift bead shape and adhesion
- Heat from nearby components may lower apparent viscosity during application
- Dense layouts can redirect flow into hidden spaces under part edges
- Board orientation between dispense and cure can affect creep
When a project involves battery electronics or power assemblies with tight clearances, it can help to review broader insulation design choices together with application control. For related system-level considerations, see how to choose an insulation adhesive for battery packs.
How Dispensing Pattern, Shot Size, and Cure Time Influence Spread
Material selection and process setup cannot be separated. The same adhesive may perform acceptably with one nozzle, pattern, and cure sequence but fail with another.
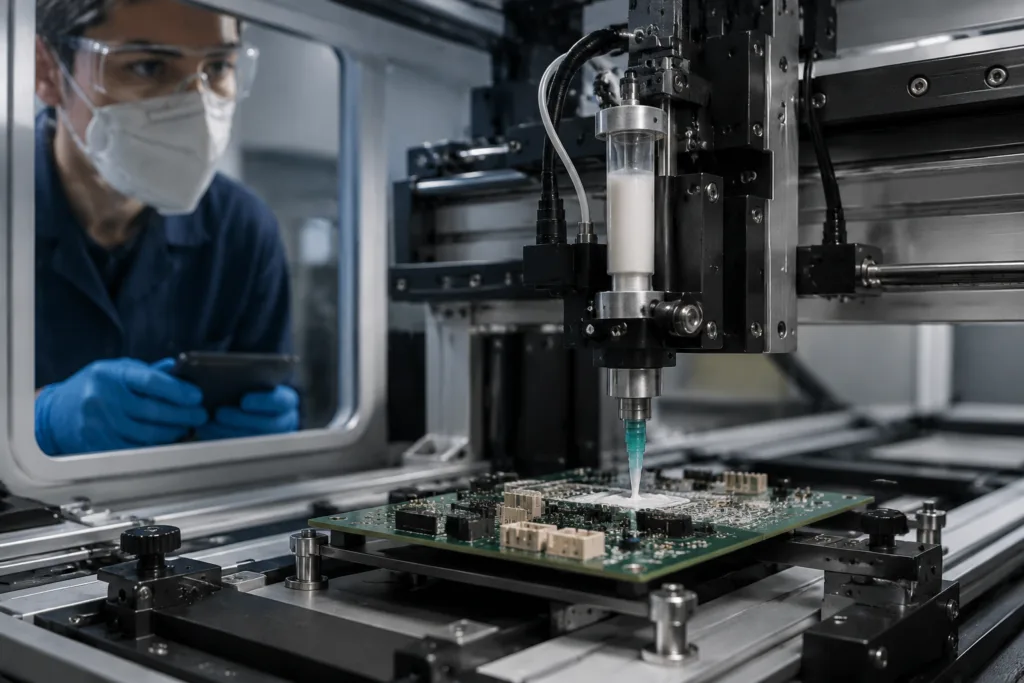
Key process variables include:
- Dispensing pattern: dots, lines, fillets, partial frames, and closed dams each produce different flow fronts.
- Shot size: excessive volume increases hydrostatic pressure and promotes outward creep; too little can leave discontinuous coverage.
- Nozzle size and speed: these affect shear during application and therefore immediate flow behavior.
- Time to fixture or cure: longer open time allows more leveling and more potential migration.
- Substrate temperature: warmer parts can increase spread even if the material looked stable during bench trials.
For many applications, trial work should compare not just one bead size but a practical process window. This helps determine whether the adhesive still behaves safely when normal variation occurs on the production line.
How Part Geometry, Surface Energy, and Clearance Affect Adhesive Movement
Assemblies often fail flow-control trials because buyers focus on chemistry first and geometry second. In reality, geometry strongly influences whether an adhesive stays localized or keeps moving.
Ask these questions during evaluation:
- Is the adhesive being placed in an open area or a semi-confined path?
- Are there narrow channels that could draw the material by capillary action?
- How close are nearby pads, pins, or connector cavities?
- Are there steep height changes that create gravitational slump?
- Do the surfaces differ in roughness or energy, causing asymmetrical spread?
- Will the part remain horizontal until the adhesive reaches handling strength?
These details matter because a suitable rheology for one layout may be unsuitable for another, even within the same product family.
Matching Viscosity to Application Methods
Different application methods place different demands on insulation adhesive viscosity.
Manual dispense
Manual work usually benefits from a forgiving material that can tolerate small variation in trigger force, dwell time, and operator angle. Medium or thixotropic systems are often easier to control when working near sensitive features, although actual fit depends on nozzle size and target geometry.
Automated dispense
Automation can manage tighter repeatability, but it also exposes weaknesses quickly. If the adhesive is highly shear-sensitive, the bead may look different at different machine speeds or after line interruptions. Stable rheology across the expected processing window is important.
Potting or cavity fill
For broader cavity filling, lower viscosity may be helpful for air release and full contour coverage, but uncontrolled rise into excluded areas must still be considered. If the application is closer to encapsulation than localized bonding, buyers may also need to compare insulation adhesive solutions for controlled component protection with broader system choices.
Localized bonding and edge sealing
When the goal is a precise bead, corner bond, or barrier around a component, higher body or thixotropy can be beneficial. The trade-off is that surface wetting and void control must still be verified on representative parts.
Key Performance Factors Beyond Viscosity
Viscosity helps determine process fit, but it should never be the only selection factor. The final material also needs to meet the functional requirements of the application. Depending on project needs, buyers may need to confirm:
- Electrical insulation performance such as dielectric-related properties
- Operating temperature exposure and thermal aging requirements
- Moisture, condensation, or splash resistance
- Mechanical flexibility versus rigidity under vibration or expansion mismatch
- Gap-fill behavior and shrinkage control
- Cure method, production takt time, and post-cure handling needs
- Documentation requirements from the current technical data sheet and safety data sheet
These values vary by formulation and must be checked for the selected product rather than assumed from chemistry alone.
What to Test During Sample Evaluation
Sample evaluation should mimic real production rather than relying only on coupon tests. Useful checks include:
- Edge control: how far the material spreads from the intended line or dot after a defined waiting period
- Slump resistance: whether the bead shape holds on vertical, angled, or stepped features
- Wetting: whether the adhesive actually contacts and covers all required surfaces
- Void tendency: whether trapped air remains around pins, corners, or under component edges
- Cure stability: whether shape changes continue during cure or heating
- Inspection response: whether operators or AOI systems can verify correct placement
A useful sourcing discussion often begins after these observations are documented with photos, dimensions, and process notes rather than general comments such as “too runny” or “too thick.”
What to Share with a Supplier Before Product Selection
To reduce trial cycles, buyers should provide more than the application name. A manufacturer needs enough context to narrow the rheology range and review process fit. The most helpful inputs usually include:
- Substrate materials and surface condition
- Assembly drawing or photos showing critical keep-out zones
- Target dispense area, line width, dot size, or fill volume
- Minimum and maximum gap or clearance
- Manual or automated dispense method
- Nozzle size, dispense pressure, and production speed if known
- Part orientation before and during cure
- Environmental exposure such as heat, moisture, vibration, or chemicals
- Electrical protection objective and any required documentation
- Sample quantity, validation plan, and expected purchasing format
When a project requires support comparing rheology options, process limits, or sample strategy, ZDS LTD can review those details through its adhesive selection technical support for rheology matching. In some cases, the discussion may also extend to packaging format or, where justified by the project, custom adhesive formulation for application-specific control.
How ZDS Helps Match Adhesive Rheology to Assembly Control
For insulation-focused assemblies, the most efficient path is usually a structured review rather than starting with a random sample list. ZDS LTD can work with engineering, production, and procurement teams to compare whether a lower-flow, balanced-flow, or more thixotropic approach is more realistic for the actual geometry and process window.
That review may include:
- Application and substrate discussion
- Identification of overflow risk areas and keep-out zones
- Comparison of localized bonding versus broader fill approaches
- Screening of likely chemistries and rheology profiles
- Sample planning for representative-part trials
- Review of current technical documents needed for supplier approval
- Discussion of packaging and supply expectations for pilot and production stages
The goal is not to recommend a product based on application name alone, but to narrow choices based on real constraints. If you are preparing an RFQ or technical review, share the component layout, dispense method, desired coverage, operating conditions, and any critical areas that must remain free of material.
Frequently Asked Questions
How do I know if an insulation adhesive is too low in viscosity for my assembly?
If trial parts show migration into pads, connectors, test points, vents, or hidden gaps after dispensing, the flow profile may be too mobile for that geometry or process window. Confirmation should include actual part testing at production temperature, shot size, and cure delay.
Is a thixotropic adhesive always better for protecting fine electronic features?
No. Thixotropic materials can improve bead control and reduce slump, but they may also wet difficult surfaces less easily or trap voids in tight areas. Selection should balance edge containment with coverage quality on the real assembly.
What process details should be included in a sample request?
Include substrate information, photos or drawings, keep-out areas, target bead or fill size, dispense method, nozzle details if known, cure conditions, part orientation, and the operating environment. This helps a manufacturer screen realistic rheology options.
Can viscosity alone confirm electrical protection performance?
No. Viscosity mainly helps predict dispensing and flow behavior. Electrical insulation, moisture resistance, thermal exposure, adhesion, and cure stability must also be checked in the current product documentation and validated through representative testing.
When should a project move from standard product screening to custom formulation discussion?
If standard options repeatedly miss the required balance between wetting and containment, or if packaging, cure behavior, or application-specific flow limits are unusually narrow, it may be reasonable to discuss whether further formulation review is justified after the project details are assessed.